$15.00
$15.00


 Find-R-Scopes
 Filters
 Lenses
 Cameras
 Lighting
 Accessories



In the food and beverage industry, maintaining consistent product quality, improving production efficiency and meeting strict safety standards are essential. As manufacturers increasingly rely on automated food inspection systems, selecting the right imaging components has become more important than ever. While industrial cameras, lighting and image processing software all contribute to inspection performance, machine vision lenses for food processing play a critical role in capturing the clear, detailed images needed for accurate analysis.

In the food processing industry, maintaining product quality and preventing contamination are critical to protecting consumers, reducing waste, and meeting demanding production standards. Even small foreign materials, such as plastic fragments, glass, metal, stones, or unwanted organic matter, can create significant challenges for food manufacturers.

In the food and beverage industry, packaging quality is just as important as the product inside. From verifying labels and expiration dates to detecting damaged seals and identifying packaging defects, manufacturers rely on automated inspection systems to maintain quality, improve efficiency and reduce costly production errors.

In the food processing industry, maintaining consistent product quality while meeting high production demands is essential. From sorting fresh produce to detecting contaminants and identifying defects, automated food inspection systems help manufacturers improve efficiency, reduce waste and maintain product standards.
Shop the latest products designed specifically for industrial imaging
Providing the leading optical filters, lenses, lighting, components and accessories for the machine vision industry.

Machine vision filters: a necessity, not an accessory
Enhance contrast, resolution, and repeatability in machine vision systems.

Innovative industrial camera solutions
High performance industrial cameras combining superior image quality with outstanding reliability and durability

Light that drives vision precision
Maximize inspection performance with advanced lighting solutions tailored to machine vision demands

Now Accepting Pre-Sale Orders for the NEW Find-R-Scope® SWIR-View
SWIR-View is a hand-held viewer covering a broad wavelength range of 400-1700nm. Coming soon!





The most popular products from industry leaders
Shop a wide range of products from globally recognized brands in the machine vision industry.



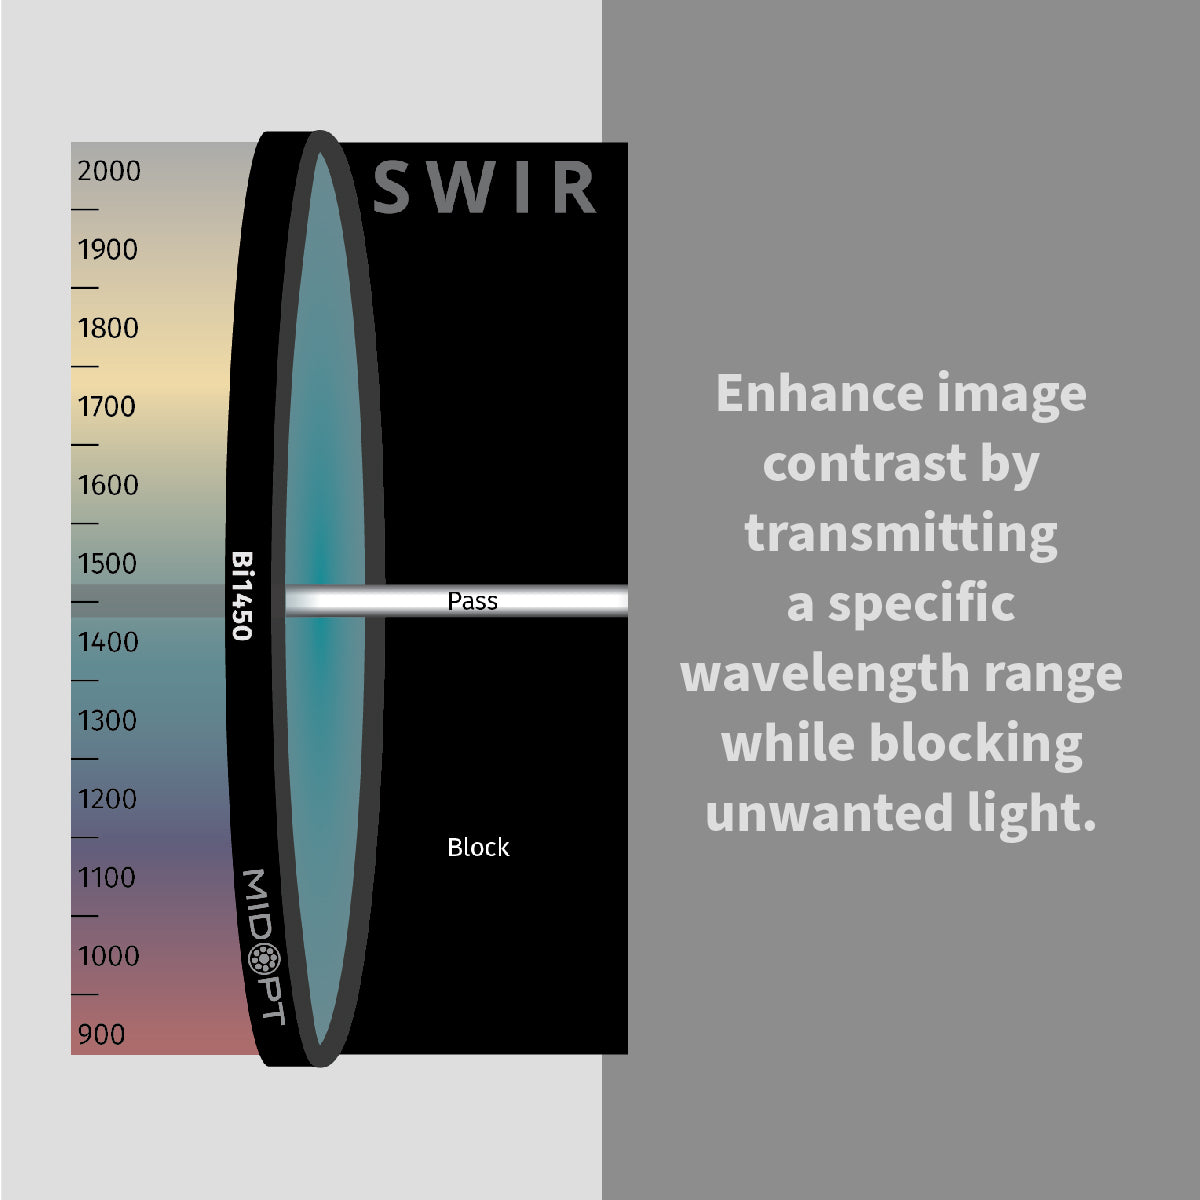
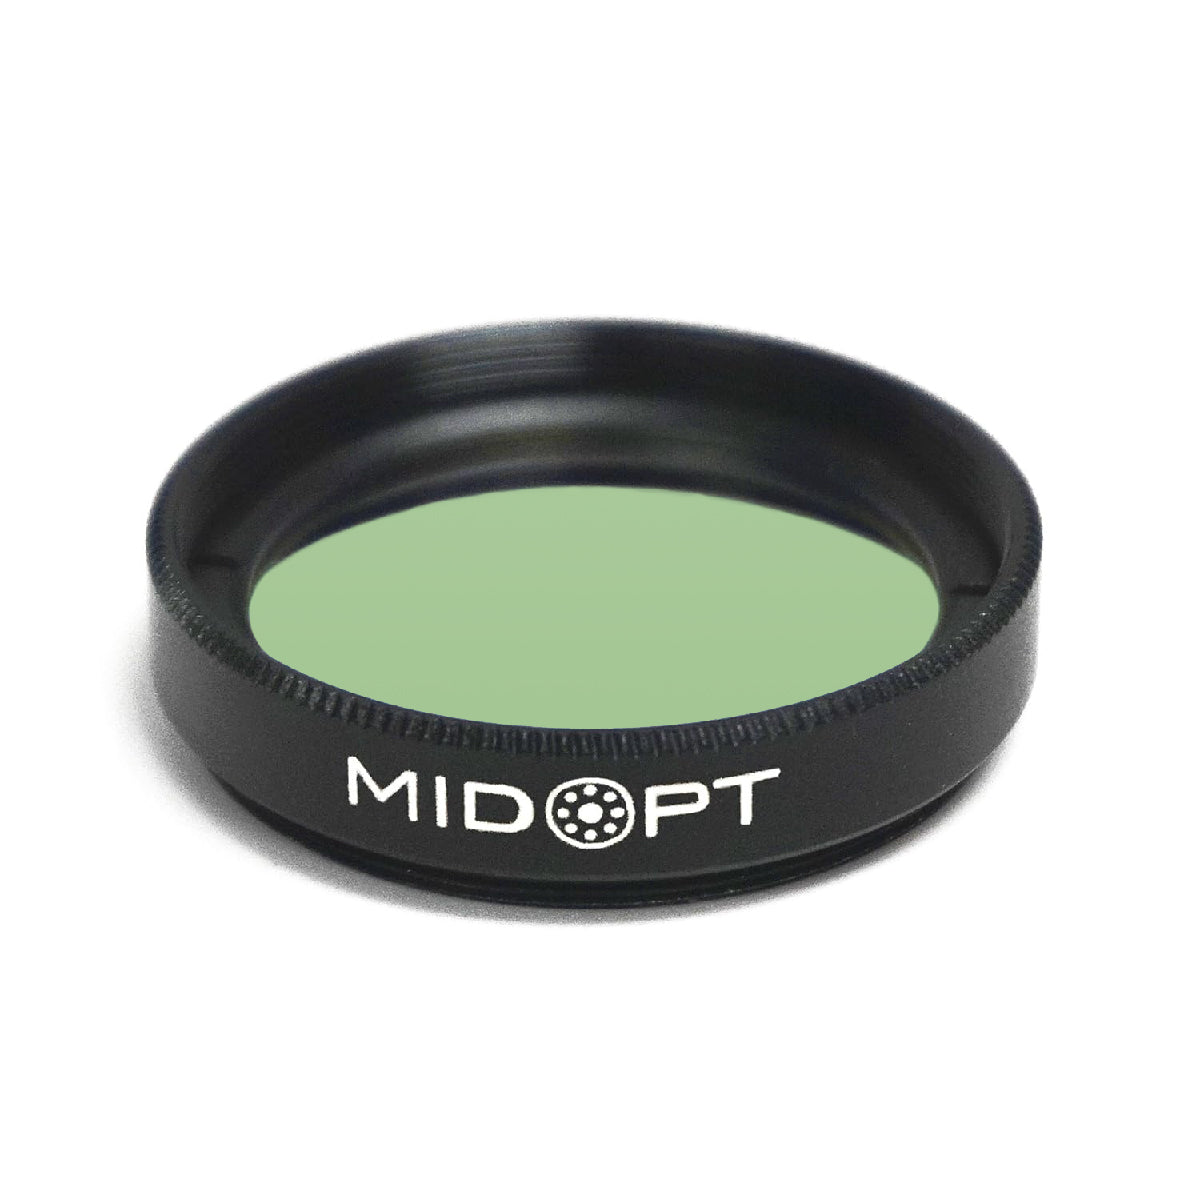
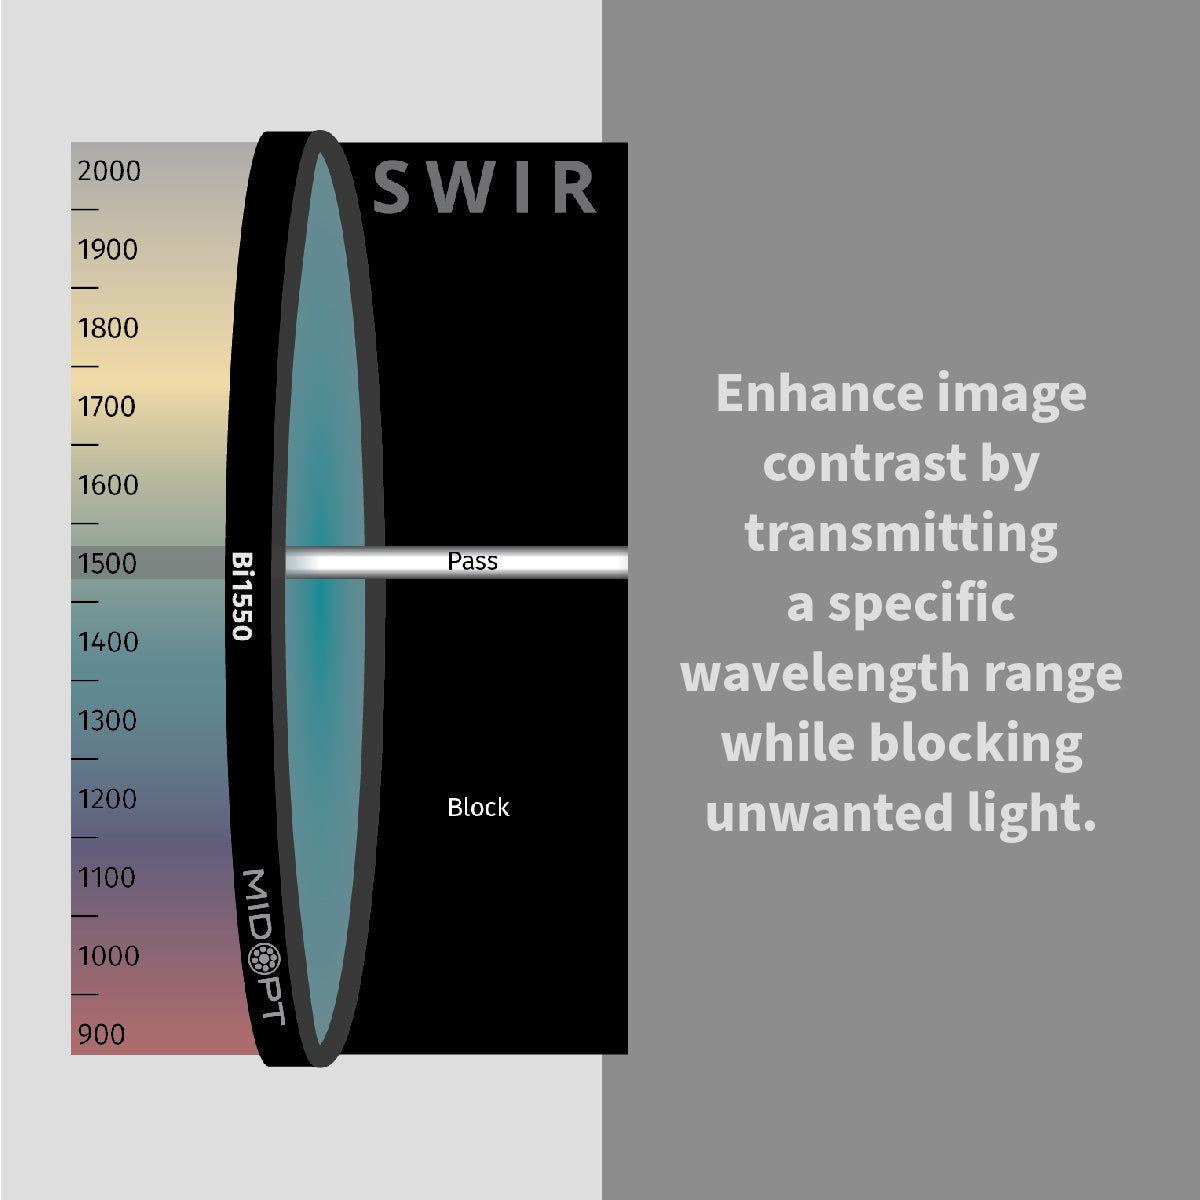
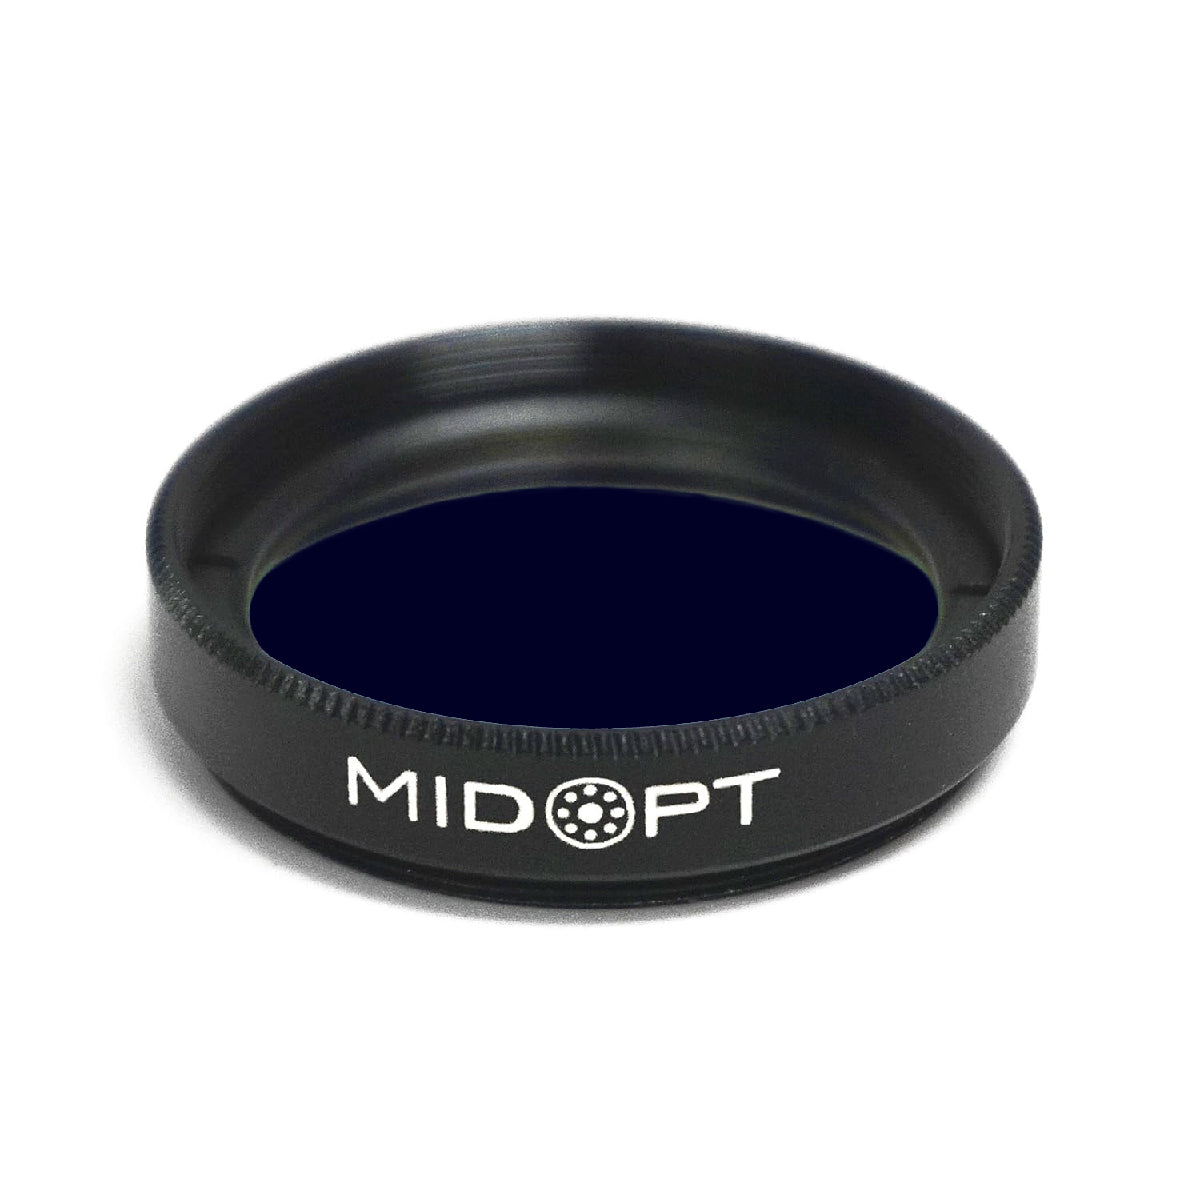
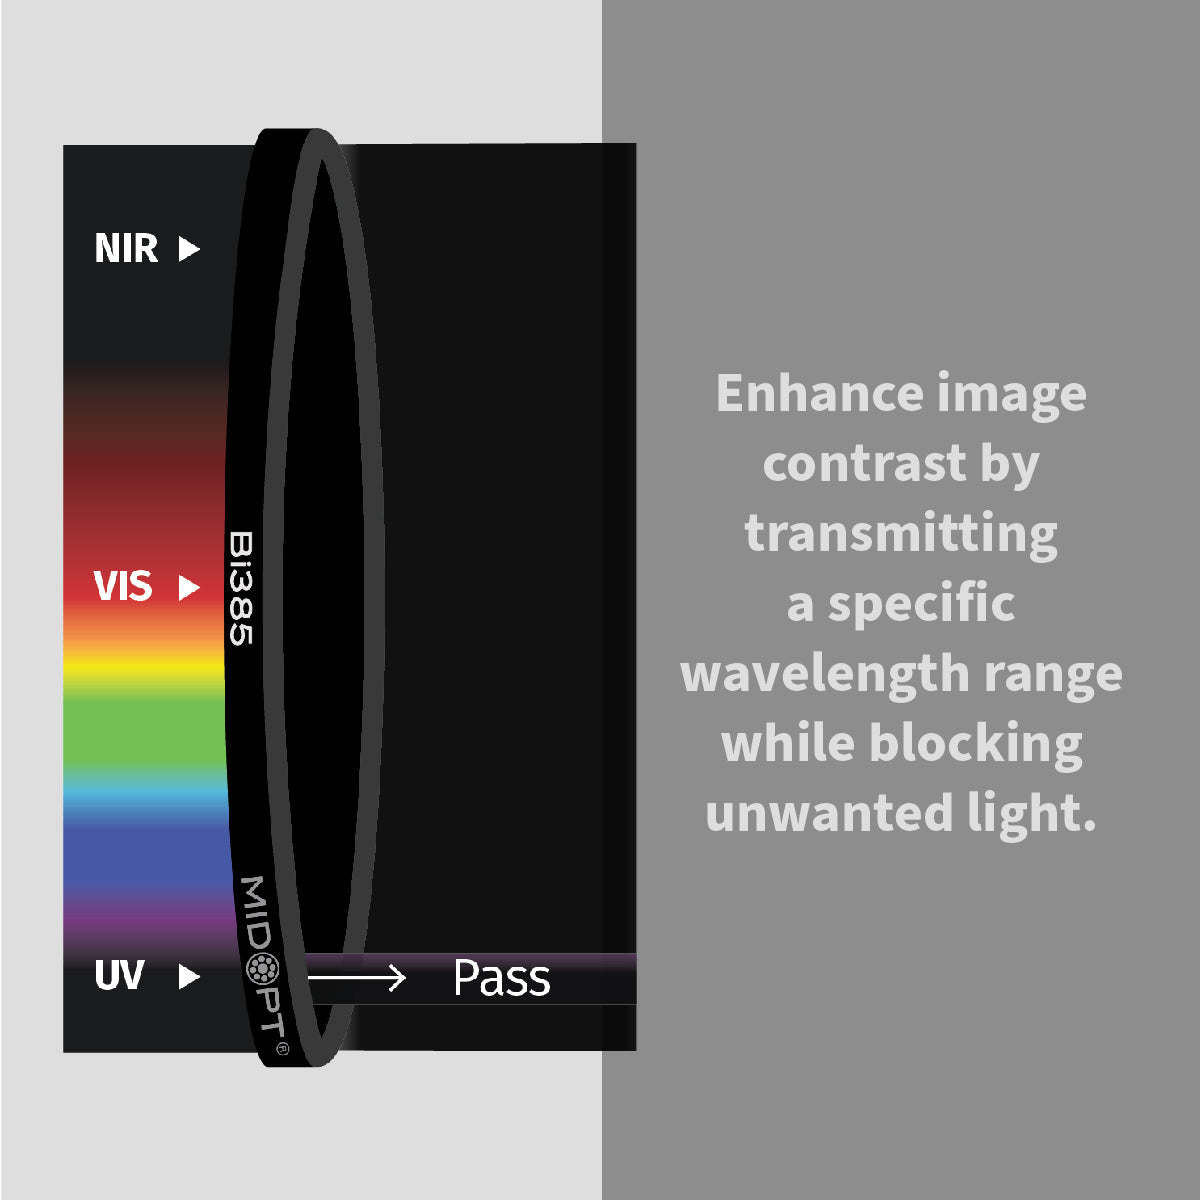
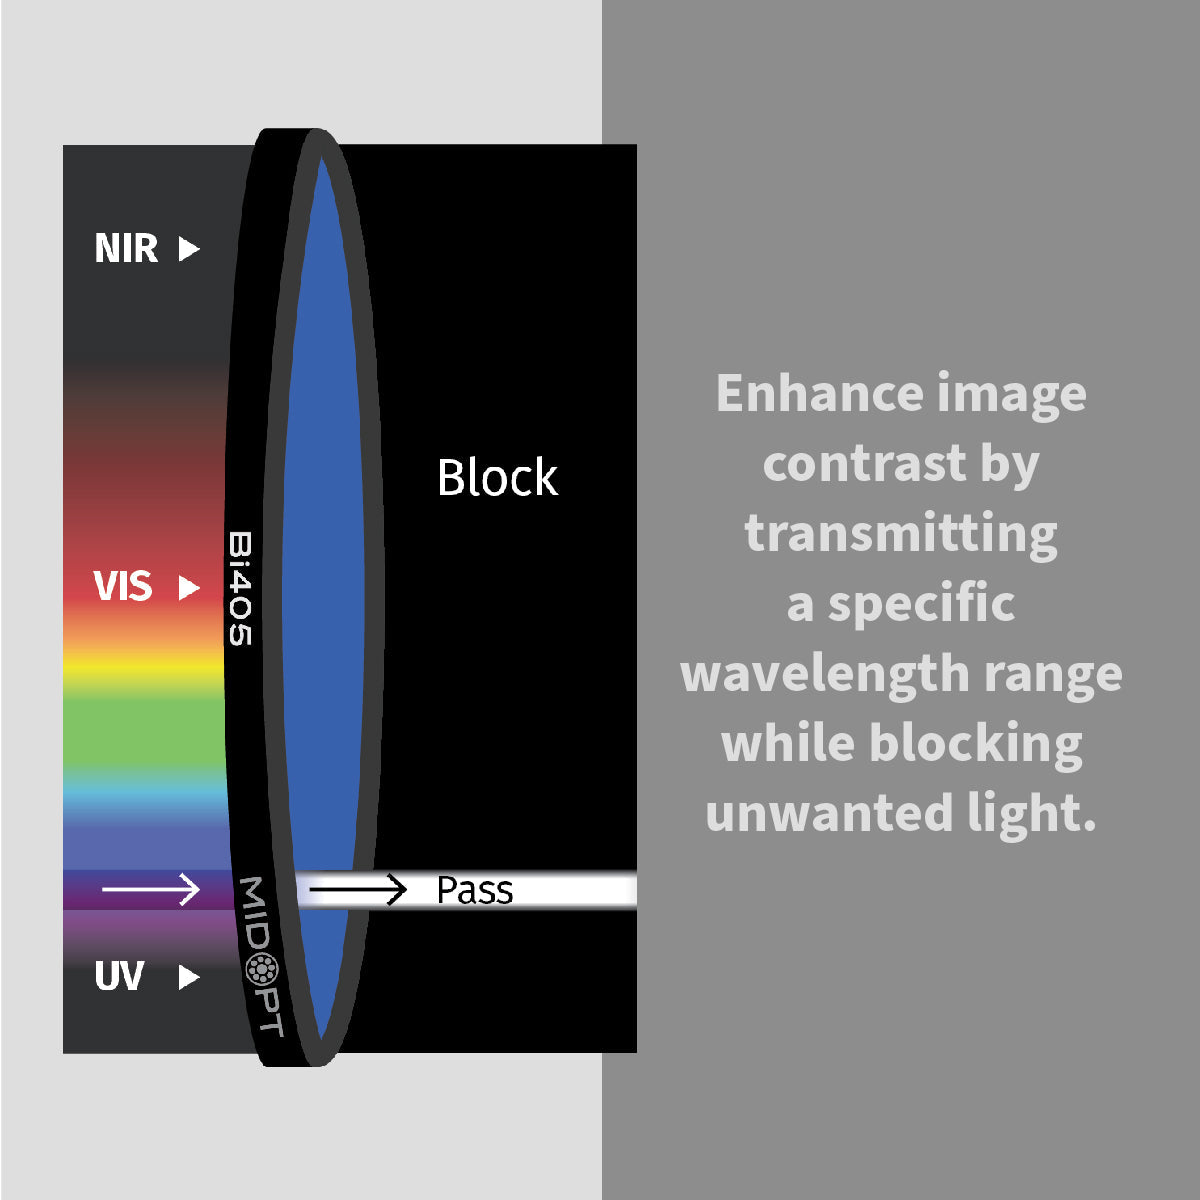
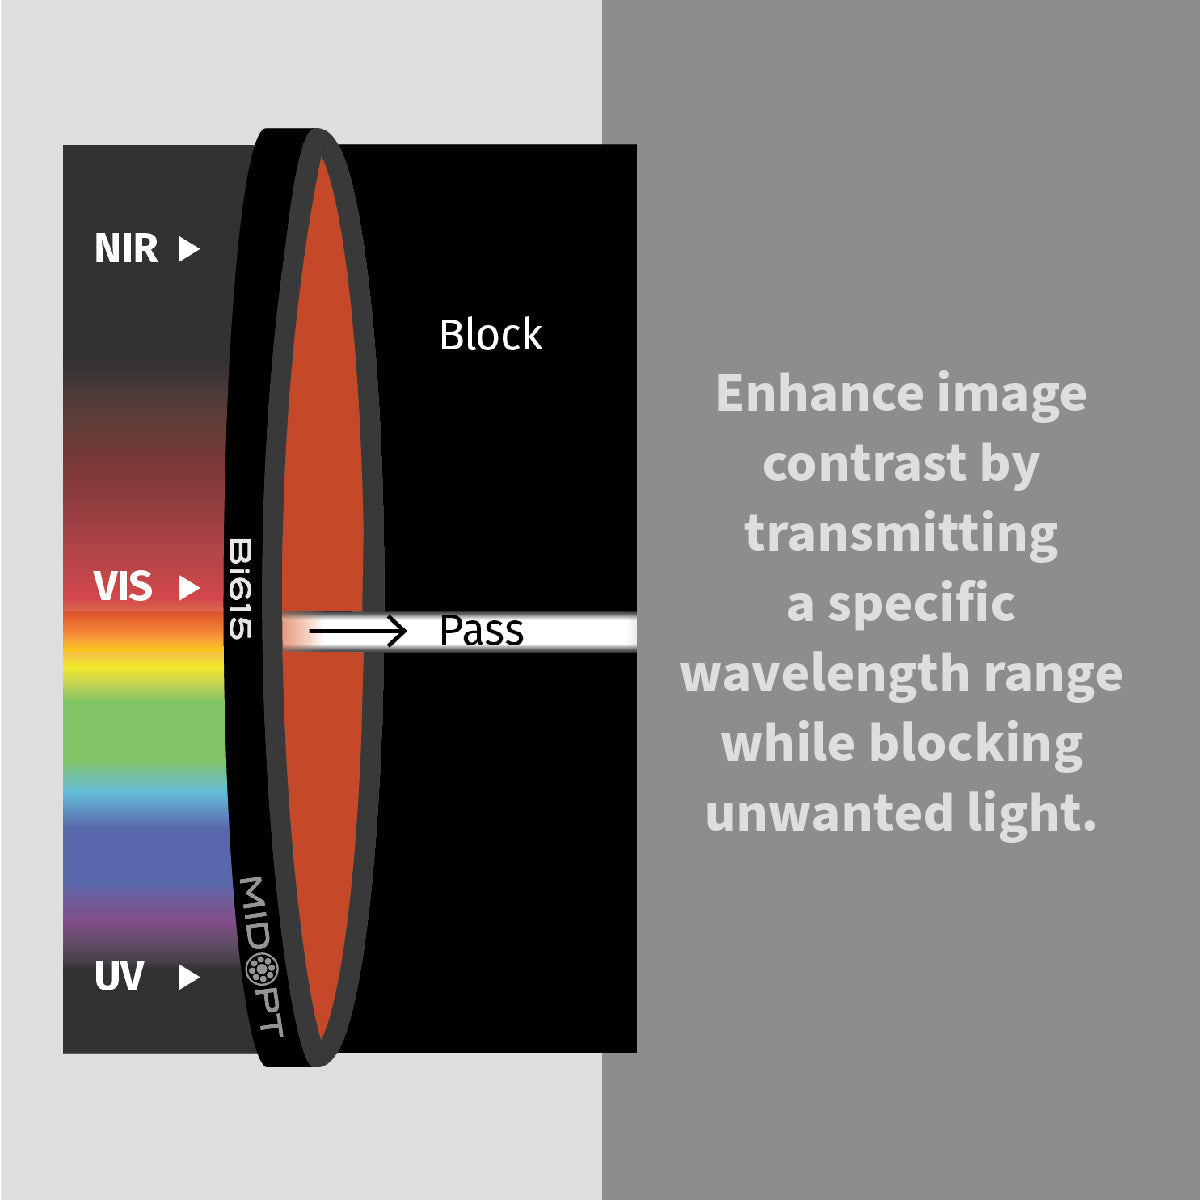
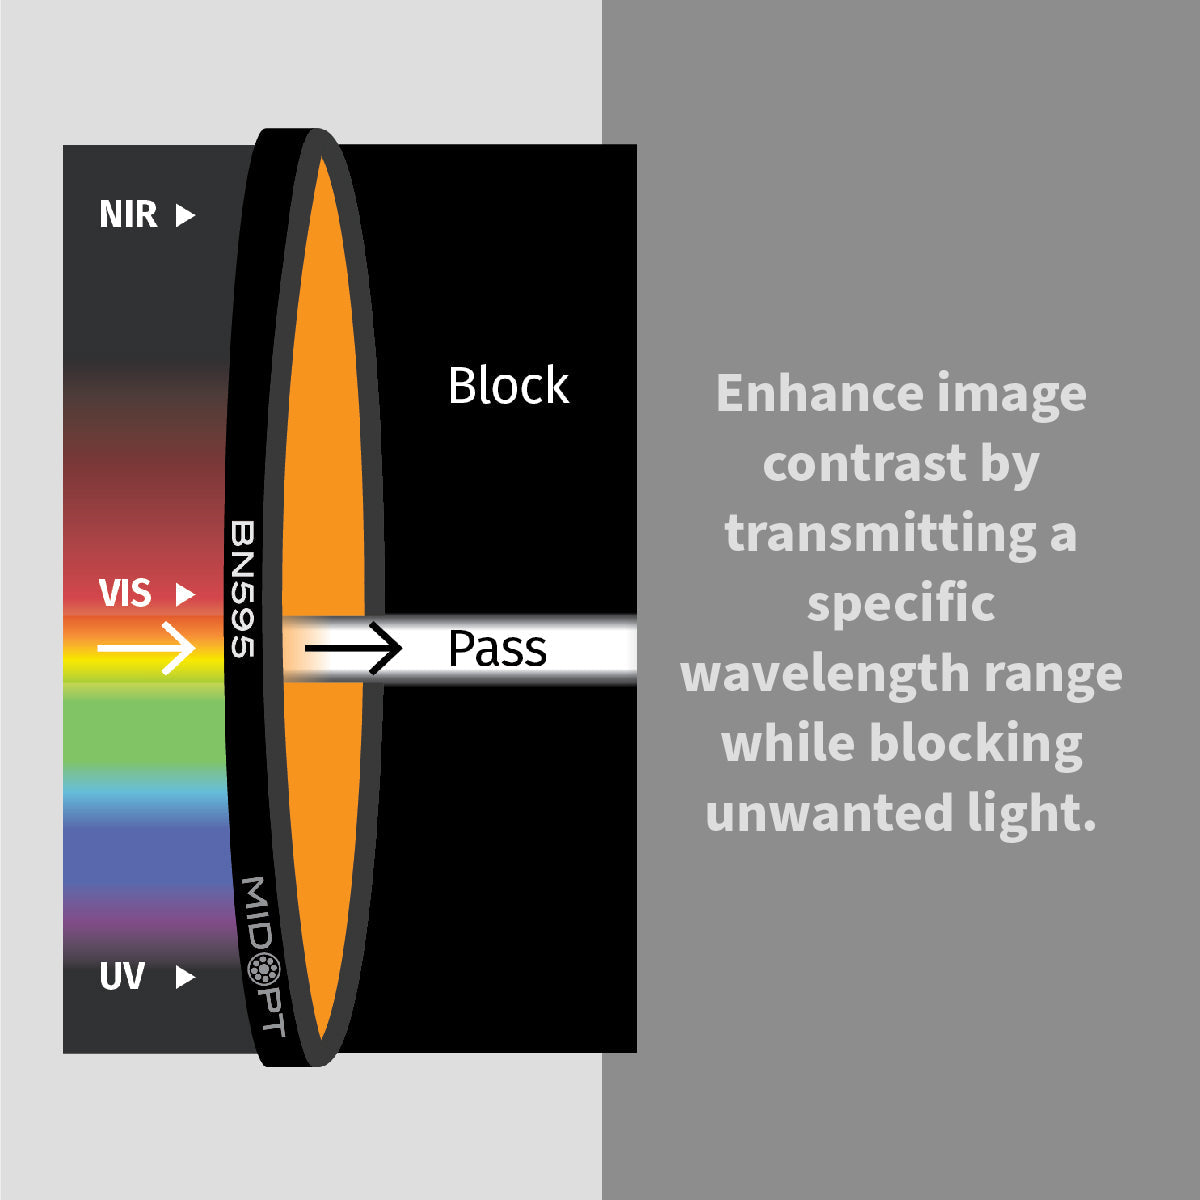
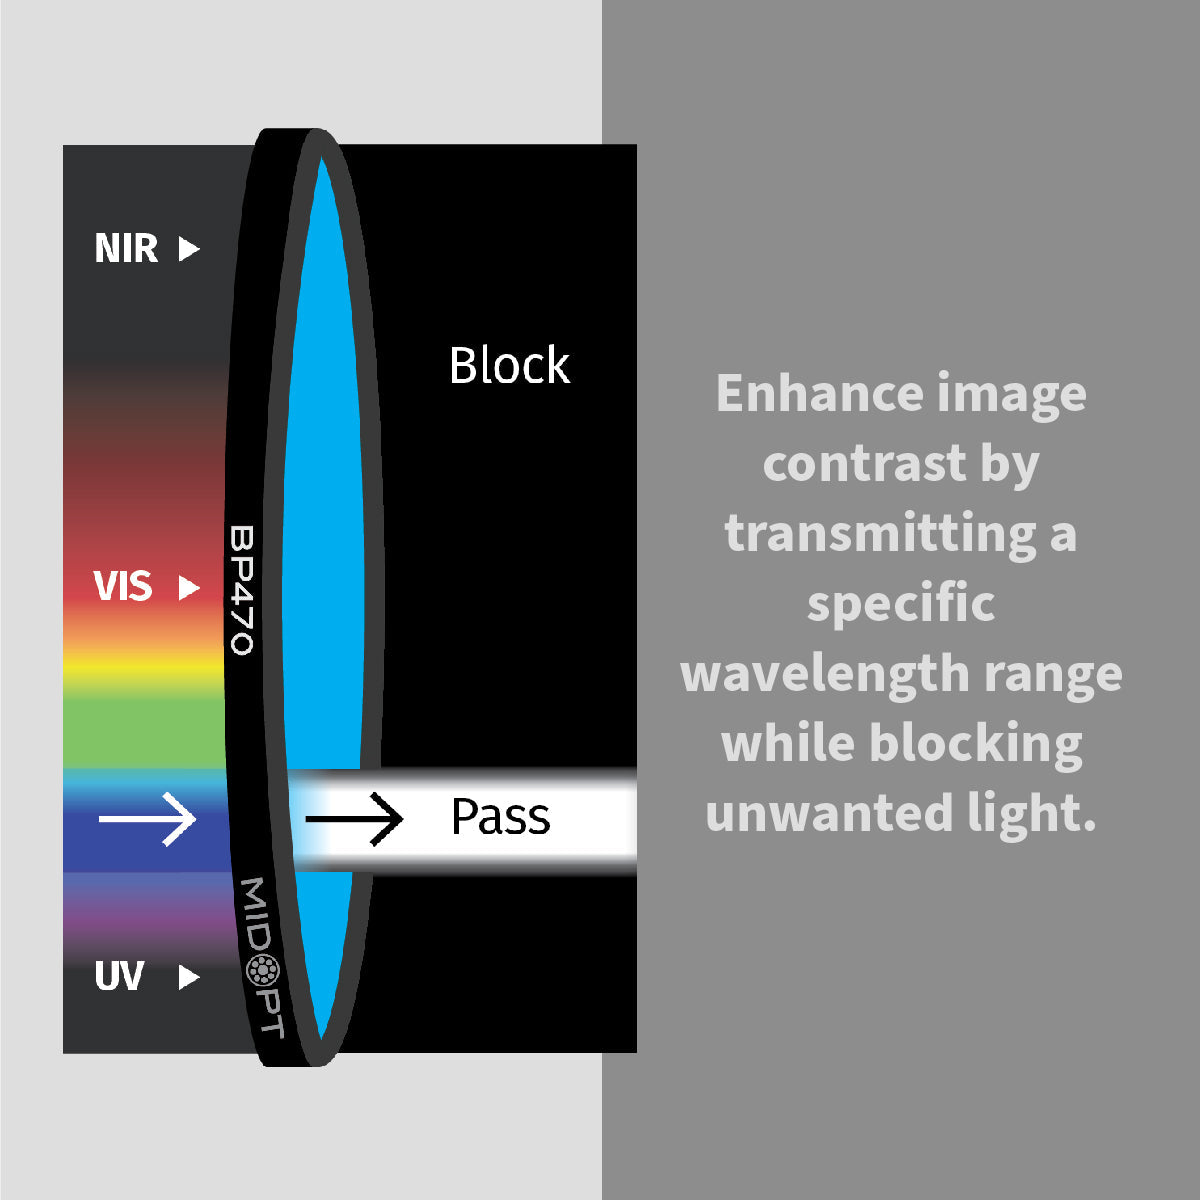
In machine vision, optical filters aren’t just add-ons, they’re essential tools for image accuracy. By carefully controlling which wavelengths pass through (and which don't), filters help maximize contrast, enhance color accuracy, highlight critical details and block ambient light that can compromise results.

In industrial imaging, choosing the right camera for a machine vision system can significantly impact performance and accuracy. One of the most fundamental decisions is whether to use a monochrome or color camera.
Optical filters are essential for achieving reliable, high-quality results in machine vision applications. They don’t just block or pass light – they enhance system performance by increasing contrast, improving color accuracy, reducing glare and isolating specific wavelengths. But not all filters are created equal.

When it comes to building a successful machine vision system, lighting is just as critical as the camera or lens. Without the right lighting, even the most advanced imaging components can produce inconsistent or unreadable results. Whether you're inspecting tiny electronics, scanning barcodes on packaging lines or ensuring quality control in manufacturing, the right lighting solution makes all the difference.

When designing a machine vision system, choosing the right lens is just as critical as selecting the right camera. A common misconception is that a photography lens can do the job. But while both lens types are engineered to capture images, machine vision lenses and photography lenses are built for very different purposes – and understanding those differences can save you from performance issues down the line.

Triple Bandpass Filters are tools that allow users to go above and beyond traditional Normalized Difference Vegetation Index (NDVI) indicators to reinvent the way crop health is monitored and to collect more information than ever before.