$15.00
$15.00

 Find-R-Scopes
 Filters
 Lenses
 Cameras
 Lighting
 Accessories



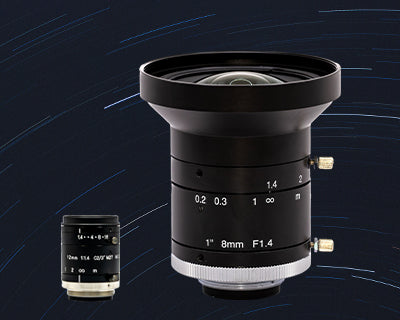
In the food and beverage industry, maintaining consistent product quality, improving production efficiency and meeting strict safety standards are essential. As manufacturers increasingly rely on automated food inspection systems, selecting the right imaging components has become more important than ever. While industrial cameras, lighting and image processing software all contribute to inspection performance, machine vision lenses for food processing play a critical role in capturing the clear, detailed images needed for accurate analysis.

In the food processing industry, maintaining product quality and preventing contamination are critical to protecting consumers, reducing waste, and meeting demanding production standards. Even small foreign materials, such as plastic fragments, glass, metal, stones, or unwanted organic matter, can create significant challenges for food manufacturers.

In the food and beverage industry, packaging quality is just as important as the product inside. From verifying labels and expiration dates to detecting damaged seals and identifying packaging defects, manufacturers rely on automated inspection systems to maintain quality, improve efficiency and reduce costly production errors.

In the food processing industry, maintaining consistent product quality while meeting high production demands is essential. From sorting fresh produce to detecting contaminants and identifying defects, automated food inspection systems help manufacturers improve efficiency, reduce waste and maintain product standards.